Case Studies
Real projects: the wastewater, the treatment train we built, and how it performed.
Industry
Showing case studies

Aircraft Landing Gear Plant: Heavy Metals Treatment
A landing gear plant expansion needed heavy metals, TSS and organics removed from 120 GPM of process water. Working from the engineers’ jar test report, we supplied the full clarifier, filtration and dewatering system.
Read the case study →
Automotive Stamping & Machining Wastewater Treatment
An international OEM parts maker sent us samples from its stamping and machining plant. In-house jar testing and a site visit produced a complete treatment train, from equalization to filter press.
Read the case study →
Bakery Wastewater Treatment System
A bakery making 75 different products needed treatment for about 75 GPM of wastewater, in a building with no single open space. We split the system between an elevated deck and the ground floor.
Read the case study →
Centralized Waste Treatment Facility
A facility that treats other companies’ waste for a fee needs flexibility. Bypasses and recombinations of separators, chemistry, DAF, filtration and a bioreactor let it handle whatever arrives.
Read the case study →
Copper & Metals Producer: Dual-Train Slant Plate Clarifier
Copper and other metals had to come out of a 200 GPM process stream. Two parallel stainless slant plate clarifier trains let the plant run full flow on either train or turn down with production.
Read the case study →
Dairy Whey Wastewater: DAF Treatment System
On-site jar testing set the chemistry for a whey producer’s 125 GPM of wastewater and CIP water. The result: a stainless DAF system with chemical pretreatment, started up and staff trained by our team.
Read the case study →
Engine Rebuilding: Oil Water Separator Packages
A worldwide engine manufacturer standardized on our separators for rebuilding shops in the US and abroad, with each OS and OSe package sized from 5 to 75 GPM and fitted to the site.
Read the case study →
Fertilizer Plant: Dual-Train DAF Treatment System
A new fertilizer plant needed process water treatment designed alongside its chemical process. We supplied dual trains of separation, flocculation, chemical metering and DAF, plus the facility layout.
Read the case study →
Flavoring & Fragrance Plant: 1,000 GPM Oil Water Separator
An international flavorings maker needed to pull natural oils and solids out of 1,000 GPM of process and CIP water. A customized FB separator with Flopak media, drum screen and access platform did the job.
Read the case study →
Food Processing: Three API Oil Water Separators
Three customized API separators now handle everything from barge wash water to flour settling for a major food producer, with tank volume that can be reused where water quality allows.
Read the case study →
Glass Container Plants: Cullet Water Oil and Solids Removal
Oils and fine glass were causing production problems at seven glass container plants. After visiting every site, we supplied separator systems for each plus piping changes to stop cullet dropout.
Read the case study →
Gold Mine Brine Water: Polypropylene Oil Water Separator
Strong brine at a gold mine rules out ordinary steel. An all-plastic OSe-36 separator on a stainless skid removes fuel oils and solids from 75 GPM of brine water.
Read the case study →
Groundwater Remediation: Vinyl Chloride Pilot with Plate DAF
A four-week pilot at an old industrial waste site proved a chemical recipe that removed iron, metals, emulsions and vinyl chloride, letting the site shut down its UV oxidation system.
Read the case study →
Groundwater Treatment: Metals and VOC Removal
Zinc, barium, lead, nickel, chrome, BTEX and solvents all turned up in groundwater at a former manufacturing site. We designed the treatment facility and supplied every piece of equipment.
Read the case study →
HVAC Manufacturing: Metals Removal with Chemical Treatment and Slant Plate Clarifier
Metals, solids and emulsions in an HVAC manufacturer’s production water called for chemistry first. Lab and on-site jar tests led to a ChemClear CT and slant plate clarifier system with dewatering.
Read the case study →
Valve Manufacturer: Machining Coolant Batch Treatment
Machining coolant mixed with cleaning and paint solutions used to be treated by hand. An automated batch treatment system now handles 750+ gallons a day for sewer discharge with far less labor.
Read the case study →
Locomotive Rebuilding: Wash Water Treatment System
Engine and chassis wash water at a locomotive rebuilder carried oils, fuels, metals and organics. A 70 GPM train of separation, chemistry, DAF and filtration treats it before discharge.
Read the case study →
Meat Processing: Grease Interceptor and DAF for Cooking Water
A brisket cooking line produced 650 gallons of fats, oils and grease water every 90 minutes. A continuous batch system built around our GTI grease interceptor and a DAF now cuts the FOG load to sewer.
Read the case study →
Military Vehicle Wash Rack: Four-Bay Wash Water Treatment
Four parallel wash bays at a Marine base in South Korea each run a container-mounted VEW system at 50 GPM, with Mudblasters, recycle pressurization and central controls.
Read the case study →
National Park Maintenance Facility: Vehicle Wash Water Recycling
A remote national park maintenance shop wanted to reuse its wash water. Jar testing, chemical pretreatment, a Clarisep and ZeoMaxx filtration now recycle about 15 GPM for washing.
Read the case study →
Naval Base Bilge Oily Water Treatment Facility (BOWTS)
A shore-side facility at a large naval base treats 250 GPM of bilge and tank runoff water using our integrated BOWTS design, from tanks and pumps to chemical metering and controls.
Read the case study →
Power Plant Cooling Water: Concrete Oil Water Separators
A power plant discharging cooling water to a river wanted protection against rare oil spills. Two gravity-flow concrete separators with Flopak media packs handle 4,000 and 9,600 GPM streams.
Read the case study →
Produced Water Disposal Plant: 1,000 GPM Oil Water Separator
Before produced water from fracking is deep well injected it is treated and tested. An OS separator with pumpouts and datalogging controls handles 1,000 GPM continuously at this disposal plant.
Read the case study →
Shipbreaking Wastewater Treatment
Breaking up ships for scrap releases bunker fuel, diesel, solids and metals. An equalization tank and OS-64 separator handle the variable load at 110 GPM before filtration.
Read the case study →
Solar Farm: Heat Transfer Fluid Separation
Therminol heat transfer fluid acts like oil at some temperatures and a solid at others. Lab testing pointed to our OSe separator, which took the oil content from 1,700 mg/L down to 2.4 mg/L.
Read the case study →
Tank Farm Stormwater, Indonesia: 1,800 GPM Oil Water Separator
Stormwater and tank bottom water at a petroleum tank farm in Indonesia now runs through an OS-720 separator sized for 1,800 GPM, with startup and training from our team.
Read the case study →
Tank Terminal Stormwater: 10,000 GPM Corrugated Plate Interceptor
An international tank terminal needed 10,000 GPM of oil separation. Our TPi design was built as a ten-channel concrete interceptor with wave plate packs and adjustable rotary skimmers.
Read the case study →
Truck Wash: Decane and Octadecane Removal
Years after we installed its separator, a waste hauler’s truck wash found decane and octadecane in its water. ZeoMaxx AC830 filtration brought them to non-detect levels.
Read the case study →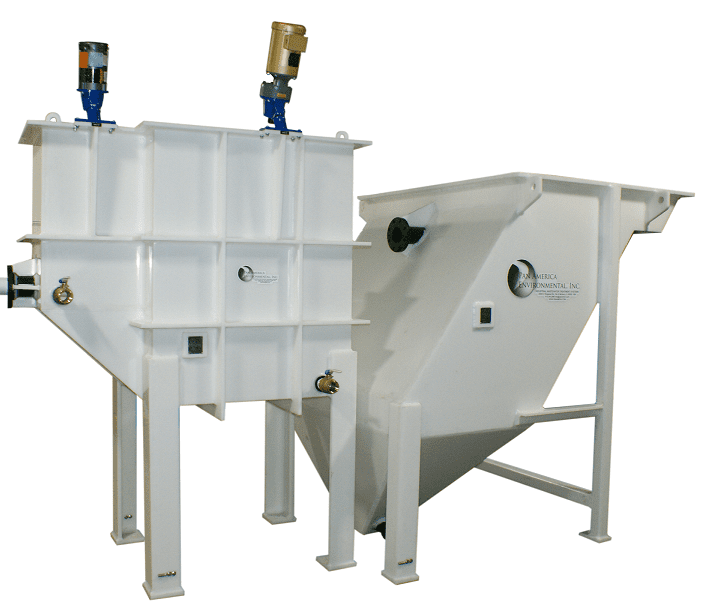
Uranium Mine Water: Polypropylene Slant Plate Clarifier
Corrosive uranium mine water needed metals and minerals removed. We built the clarifier and pretreatment in polypropylene and paired them with a polypropylene OSe separator for oils and fuels.
Read the case study →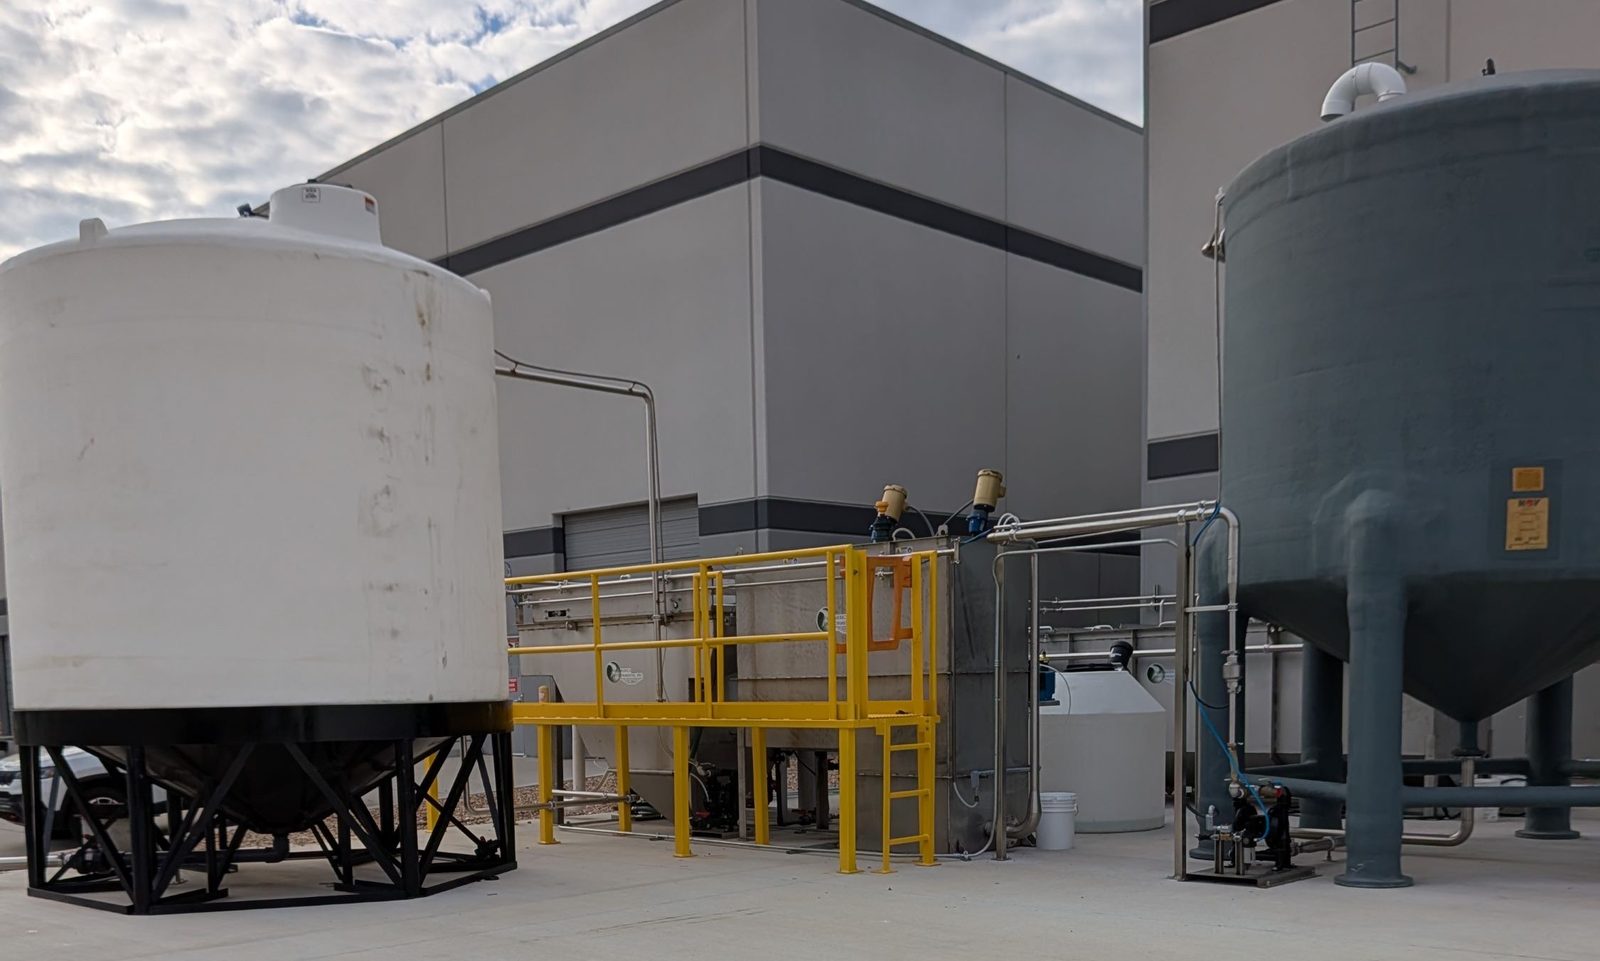
Prepared Foods Manufacturer: Grease Interceptor, Chemical Treatment and Plate DAF for Prepared Foods Wastewater
A specialty prepared and frozen foods plant needed to meet municipal sewer limits for FOG, TSS, BOD and COD. A Pan America pretreatment train of a GTI grease interceptor, ChemClear CT chemical treatment and a PD-50 plate DAF now handles its high-strength process water.
Read the case study →
Vegetable Processing: API Separator for Solids Removal
Potato and broccoli pieces were the problem at a large vegetable processor. An API250 separator with sludge auger and skimmer now removes both floating and sinking solids at 150 GPM.
Read the case study →
Wood Pole Preservation Solution Treatment
Preservation solution waste at a utility pole plant separates into three layers in one tank. Our PLC system detects each layer as the tank drains and changes the chemical dose to match.
Read the case study →Tell us your flow rate and what's in the water
Our engineers size and configure each system for your facility. Call 262.716.0105 or send the details and we'll follow up with a recommendation and pricing.